
Drilling a hole for rivetnuts
Discussion


I need to drill a 10mm hole into sheet steel for a rivet nut.
Any tips for getting a perfectly round hole? Hand drills and 10mm bits (even decent cobalt ones) usually produces a nice oval hole, which the rivnut slides around in!
Am I doing something wrong or is there a better method?
Thanks all
Any tips for getting a perfectly round hole? Hand drills and 10mm bits (even decent cobalt ones) usually produces a nice oval hole, which the rivnut slides around in!
Am I doing something wrong or is there a better method?
Thanks all
Ideally you want a sheet metal drill bit or a standard one sharpened into this configuration. See the pic under "drill bit types" on the page below. The central spike locates the bit while the o/d of the hole is drilled to size. A bit like how a hole saw works.
http://www.physics.wisc.edu/ishop/terminology.html
However other methods work fine with standard 118 degree point metal drills. Clamping a thicker piece of metal, or even an offcut of hardwood, over the hole location and drilling through that first is ideal if you have access to do so.
An old engineer's trick though is to drill through a piece of folded cloth. Get an old tea towel or face flannel, cut a 3" or 4" square out of it and fold that twice to obtain a square half the size and four layers thick. Drill a small pilot hole, put the cloth centrally over that hole, press down hard with the 10mm bit and drill through the lot at a medium speed.
The friction from the edges of the cloth rotating against the sheet metal hold the drill bit steady and prevent it from drilling the dreaded triangular hole that standard bits often produce in thin material.
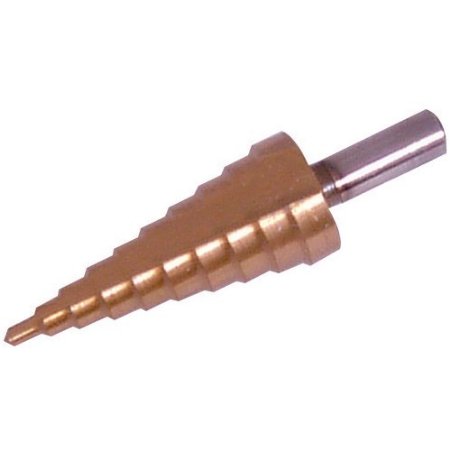
Step drills are fine but I find that one step is too small and the next too large...always happens.
I use a conical bit like these
http://uk.safestb2b.com/3-pieces-of-free-cone-dril...
Steve
I use a conical bit like these
http://uk.safestb2b.com/3-pieces-of-free-cone-dril...
Steve
Sure you have the correct tooling for securing the rivnuts ?
Ive used a few sizes, even ones too big for the tool ( broke the tool using them lol )
But never had an issue making them secure with a normal drill hole. That's up to an M8 size fitting, although the tool was only supposed to be up to M6
Ive used a few sizes, even ones too big for the tool ( broke the tool using them lol )
But never had an issue making them secure with a normal drill hole. That's up to an M8 size fitting, although the tool was only supposed to be up to M6
Gassing Station | Engines & Drivetrain | Top of Page | What's New | My Stuff